To achieve successful food powder processing, manufacturers must eliminate flow stagnation, product cross-contamination, and structural recipe breakdown. Traditional gravity-fed production systems fail to discharge complex mixtures uniformly, leading to costly plant downtime. The primary solution is investing in advanced food powder handling equipment, such as Matcon’s Intermediate Bulk Container (IBC) systems fitted with patented Cone Valve technology. This setup guarantees seamless mass flow, isolates dust, and automates transfer pathways to maintain rigorous food safety standards.
By decoupling manufacturing steps like formulation, mixing, and packing, Matcon’s hygienic handling architecture empowers food facilities to boost overall equipment effectiveness (OEE), eliminate batch cross-contamination, and manage volatile recipe variations dynamically.
What Are the Critical Challenges in Food Powder Handling?
Managing raw food ingredients introduces distinct physical and structural variables. Unlike predictable liquids, bulk food powders possess contrasting bulk densities, varied cohesive properties, and diverse particle scales.
When processing systems rely on fixed, non-agile line configurations or standard butterfly valve storage bins, several material bottlenecks inevitably surface:
- Blend Segregation: Recipes containing items of disparate weights, such as baking premixes or protein supplements, often separate during standard discharge. Heavy granules drop faster while smaller elements trail behind, altering recipe balance.
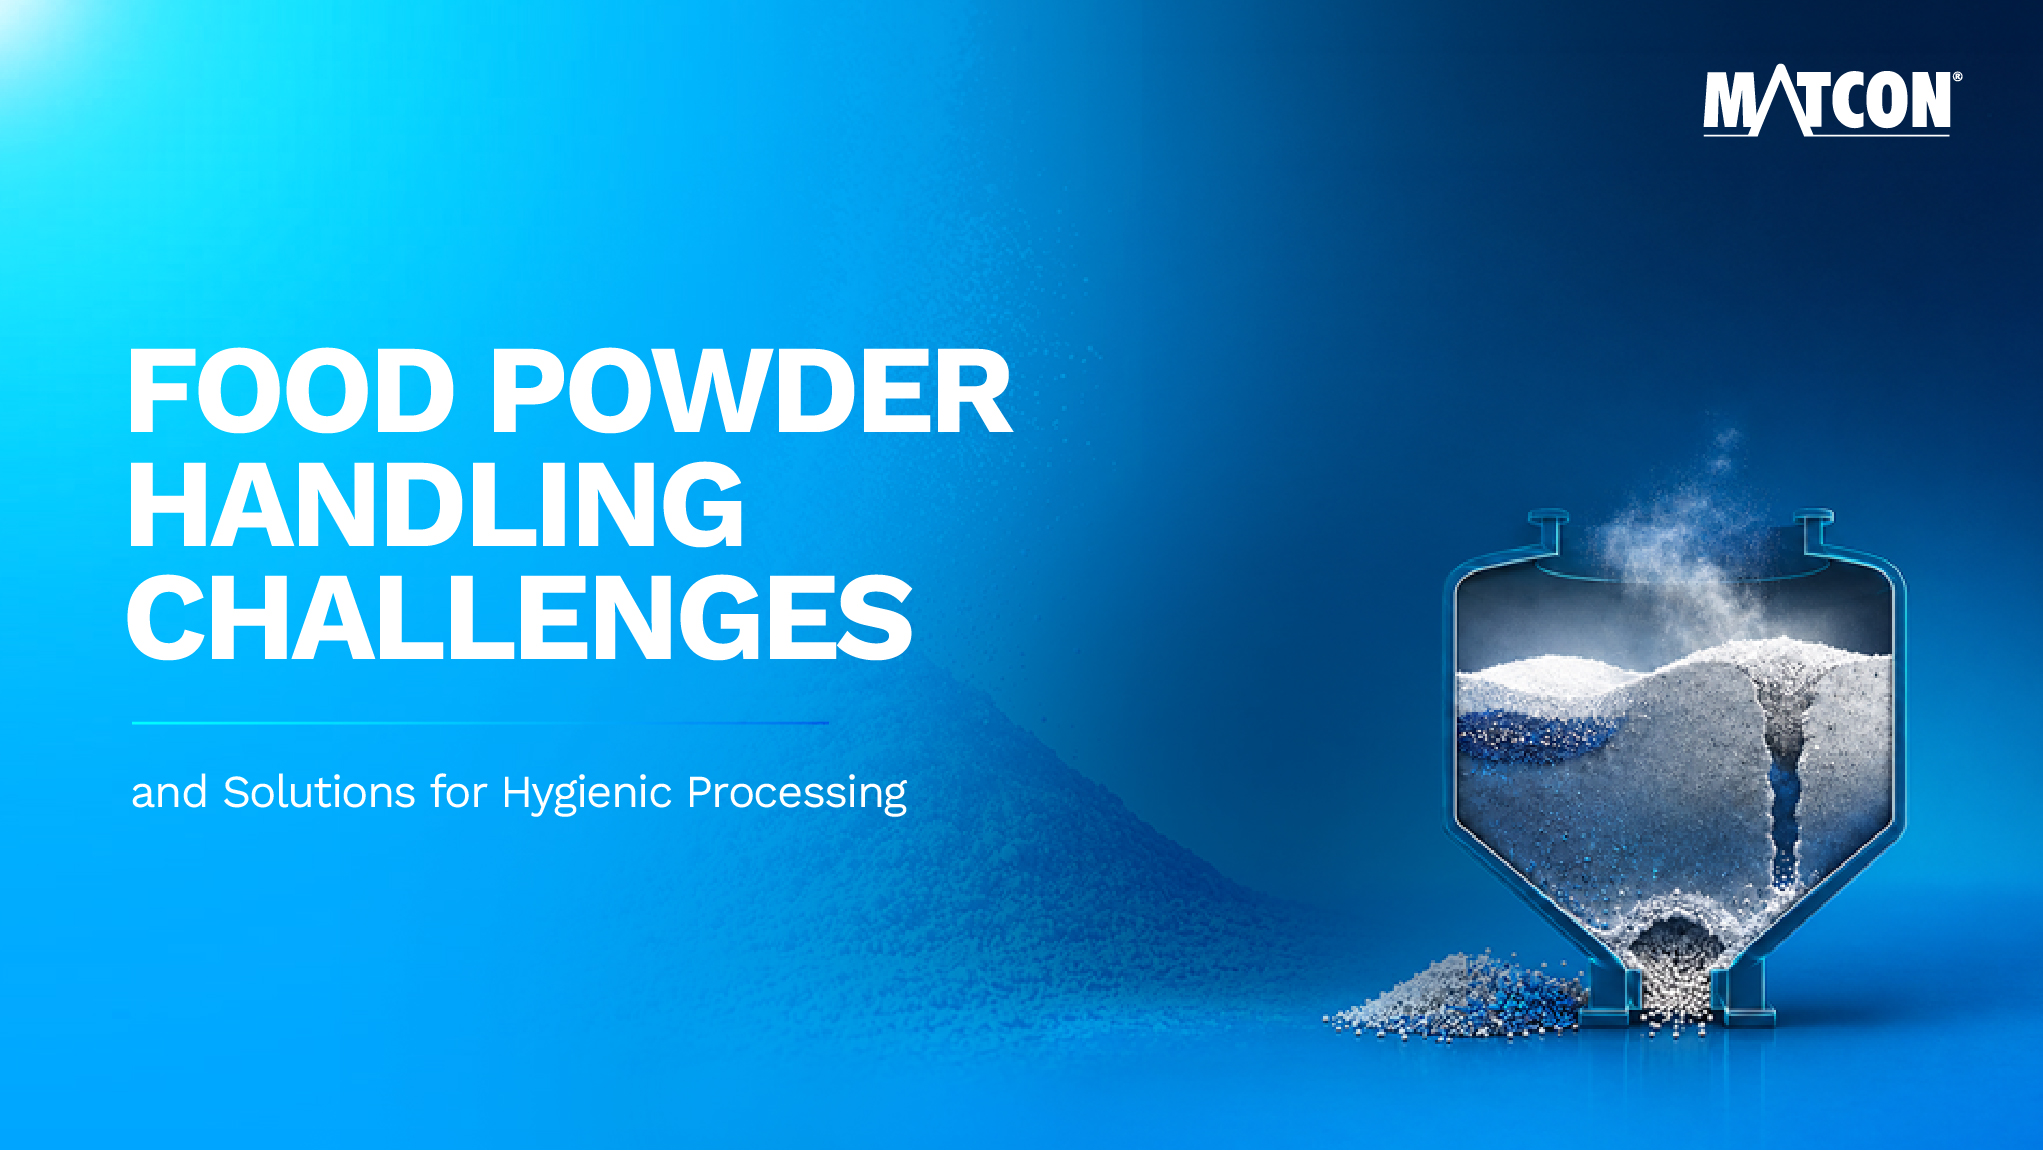
- Ratholing and Bridging: Sticky, cohesive, or ultra-fine food powders create structural bridges or empty internal vertical “ratholes” across the discharge opening, starving downstream packaging lines.
- Cross-Contamination Risks: Handling varied allergen profiles (such as gluten or dairy derivatives) inside a rigidly connected pipe network requires extensive manual cleaning windows, creating substantial operational bottlenecks.
- Dust Accumulation: Uncontained material handling coats processing floors, presenting operator health hazards and increasing combustion risks.
For processing plants dealing with liquids rather than bulk solids, implementing heavy-duty air-operated double diaphragm pumps or reliable industrial internal gear pumps from sister IDEX brands like Warren Rupp or Viking Pump handles fluid movement safely. However, managing dry bulk solids efficiently requires purpose-built food powder handling equipment capable of optimizing material dynamics without sacrificing hygiene.
How Does Matcon Cone Valve Technology Prevent Blend Segregation and Ratholing?
To counter traditional flow disruptions, Matcon invented the patented Cone Valve Technology. Placed securely at the base of every Matcon Intermediate Bulk Container (IBC), this pneumatically operated system alters how raw ingredients discharge.
Instead of opening a central core path that causes material to roll and separate, the Matcon Cone Valve lifts vertically within the bin body. This action forms an even, annular gap around the container perimeter.
Consequently, the entire bulk mass travels downward in a uniform, controlled first-in, first-out sequence. The lifting motion also provides deliberate, direct mechanical agitation to the core of the recipe mix, breaking down any internal bridging before ratholes can form.
Why Is Parallel Processing Essential for Food Processing Automation?
Modern food manufacturing requires high flexibility to handle expanding product catalogs and changing flavor choices. Traditional coupled lines link formulation, blending, and packing steps directly together, meaning a single recipe changeover stalls the entire facility for cleaning.
Decoupling with Matcon IBC Systems
Matcon’s advanced food processing automation uses standalone IBC structures as the primary vessel for every individual manufacturing phase. The recipe is formulated directly into the IBC, mixed inside an off-line container blender, transported seamlessly to the packaging line, and cleaned inside an automated wash station.
| Processing Attribute | Coupled Traditional Lines | Matcon Automated Parallel Processing |
|---|---|---|
| Operational Workflow | Fixed, sequential line paths. | Independent, parallel operations. |
| Changeover Downtime | Highly intensive manual line washing. | Instant in-bin swapping with zero blender cleanup. |
| Allergen Control | High cross-contamination risks. | Complete, dust-tight product containment. |
| Overall Equipment Effectiveness | Constrained by the slowest single stage. | Maximized via constant asset use. |
Key Applications: Where Matcon Powder Transfer Systems Transform Operations
Matcon’s specialized powder transfer system architectures provide measurable process improvements across critical food and beverage sectors:
1. Sports Nutrition and Milk Powders
Infant formulas and sports supplements contain vital micro-ingredients, vitamins, and high-density proteins. Matcon IBC systems protect blend consistency from the initial mixing stage straight to the dosing station, guaranteeing that every packaged serving matches the exact nutritional label.
2. Flavorings and Food Seasonings
Seasoning mixes often blend highly cohesive, oil-heavy components alongside granular salts. Matcon’s robust Cone Valve discharge systems break the sticky material bonds that typically choke traditional drop-feed lines.
3. Industrial Bakery Premixes
Handling high volumes of flour, sugar, and active enzymes creates airborne dust risks. Matcon provides a fully sealed, closed-path hygienic handling environment that safely isolates allergens and minimizes airborne particulate risks.
How to Select the Right Hygienic Food Powder Handling Equipment
When investing in new equipment for your plant, focus on these critical design factors:
- Material Construction and Geometry: Choose high-grade 316L stainless steel with ultra-smooth internal profiles that eliminate product-trapping crevices.
- System Integration and Automation: Verify that the containers pair cleanly with automated guided vehicles (AGVs) and central plant monitoring networks.
- Validated Cleaning Protocols: Look for systems that support efficient clean-in-place (CIP) operations or structured wash cabinets to minimize water consumption and downtime.
Contextual Safety Note: When monitoring your automated processing floor’s electronic networks, consider using heavy-duty industrial grounding straps or durable cable cleats from brands like BAND-IT to keep high-voltage electrical pathways organized and safely secured in high-vibration washdown environments.
Conclusion: Safeguarding Your Product Quality with Matcon by IDEX MPT
Maintaining hygienic process control requires production equipment that effectively eliminates material handling bottlenecks. Choosing Matcon’s engineered food powder handling equipment protects your valuable recipes from blend segregation, eliminates ratholing issues, and prevents cross-contamination across your plant.
As part of the IDEX Material Processing Technologies (MPT) division, Matcon leverages decades of specialized bulk solids processing experience. Our local manufacturing center in Sanand, Gujarat, offers premium global engineering standards with rapid delivery timelines and dedicated local maintenance support. Partner with Matcon to future-proof your food production facility today.